Dynamics 365
 Power Platform
 Dynamics
 Cloud & Productivity
Business Central for medical device manufacturers: Traceability, quality, and compliance

Medical device manufacturers need to trace materials through production, manage quality inspections and nonconforming inventory, and respond quickly to quality issues or recalls. Business Central for medical device manufacturers connects manufacturing, inventory, quality management, warehousing, sales, and finance in one medical device ERP environment. Lot and serial tracking also helps manufacturers follow materials and finished devices through the supply chain.
Business Central can support the records, controls, and workflows behind a compliance program, but the software alone does not make an organization compliant with FDA, Health Canada, ISO 13485, or other medical device requirements.
Quick answer: Can Business Central support medical device manufacturing?
Yes. Business Central can support small and midsize medical device manufacturers that need to connect production, inventory, lot and serial traceability, quality inspections, purchasing, warehousing, sales, and finance. It can also support many records and operational controls used in regulated manufacturing. However, Business Central is an ERP platform, not a complete replacement for every eQMS, MES, labeling, document control, or regulatory application a manufacturer may require.
What is Dynamics 365 Business Central?
Microsoft Dynamics 365 Business Central is Microsoft’s cloud ERP for small and midsize organizations. It brings financial management, purchasing, sales, inventory, warehouse operations, supply planning, reporting, and other core business processes into one system.
Medical device manufacturers that want to use Business Central’s manufacturing functionality need Business Central Premium licenses. Premium includes everything in Business Central Essentials plus manufacturing and service management. Manufacturing capabilities include production orders, production BOMs, routings, work and machine centers, capacity planning, material consumption, production output, and costing.
For a medical device manufacturer, this allows the ERP to connect processes across departments. A component received from a supplier can carry a lot number into inventory, move into production, become part of a finished device, pass through quality inspection, and eventually ship to a customer while the related operational and financial transactions stay connected. Manufacturers evaluating the platform can explore additional Business Central manufacturing capabilities, including production planning, materials, capacity, inventory, and costing.

What do medical device manufacturers need from an ERP system?
Medical device manufacturing adds controls that many general manufacturers do not manage at the same level. When evaluating a medical device ERP, manufacturers should look beyond accounting and production scheduling.
Important requirements can include lot and serial traceability, component-to-finished-device genealogy, quality inspections, controls for nonconforming inventory, expiration tracking, production history, distribution records, recall readiness, and auditability.
The ERP also needs to connect these requirements to everyday operations. Quality should connect with receiving and production, traceability should continue through shipment, and finance should have accurate inventory and production cost information.
Key ERP requirements for medical device manufacturers
Medical device manufacturers should evaluate how an ERP supports each requirement and where a specialized application may still be necessary.
How does Business Central provide traceability for medical device manufacturers?
Traceability is one of the most important ERP requirements for medical device manufacturers. When a material fails inspection or a supplier reports a defect, the business needs to understand what happened before and after that material entered production.
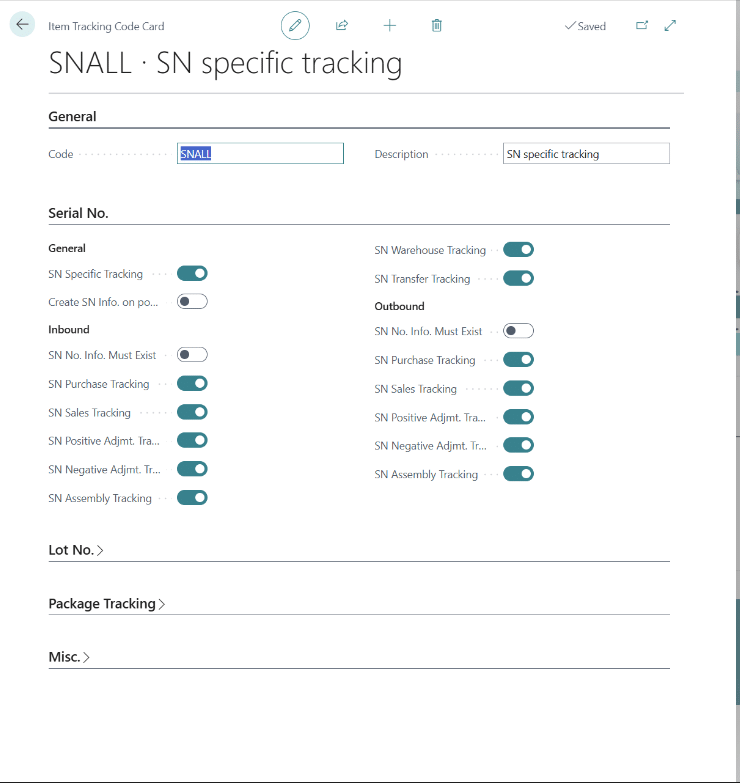
Business Central supports serial, lot, and package number tracking on inbound and outbound transactions. Its Item Tracing and Find Entries tools can follow tracked inventory forward and backward through posted transactions.
Track components and finished devices by lot and serial number
Business Central can assign and record lot or serial numbers as materials are received, produced, transferred, consumed, and shipped. Posted tracking information remains connected to the related item ledger entries.
That allows a manufacturer to build traceability across the product flow:
Supplier → Component lot → Production order → Finished device lot or serial number → Warehouse → Customer
Consider a supplier that reports a defect in Component Lot A102. The manufacturer may need to identify which production orders consumed A102, which finished-device lots or serial numbers came from those orders, whether affected stock remains on hand, and where finished products were shipped.
Business Central’s Item Tracing page can follow this transaction history forward or backward. For a broader look at stock control, locations, item movements, and tracking, see Business Central inventory management.
Connect material consumption to production output
As users post production consumption and output, Business Central records how tracked materials move through manufacturing. Item tracking details can include serial numbers, lot numbers, package numbers, expiration dates, and warranty dates. This creates an operational history connecting purchased material with the production order where it was consumed and the finished item produced from that order.
Track expiration dates when shelf life matters
Some medical device materials, sterile products, chemicals, adhesives, components, or finished products may have expiration requirements.
Business Central item tracking can associate expiration information with tracked inventory and support expiration rules when managing stock. For a practical example, see how to manage lot expiration in Business Central.
Improve recall investigations
A recall investigation puts the entire traceability design to the test. Business Central can help by linking posted inventory transactions across purchasing, production, and sales.
A manufacturer can start with a defective component lot and trace origin to usage to see where the lot was consumed, the related production output, and subsequent sales shipments. The process can also work in reverse, starting with a shipped finished product and tracing it through production consumption to the purchased component.
The Find Entries function can help identify additional records containing the affected lot or serial number, helping the manufacturer determine:
- Which supplier provided the affected material
- Which production orders consumed it
- Which finished products may contain it
- Which affected inventory remains on hand
- Which customers received finished products
- Which open records may still reference the affected lot or serial number
Business Central provides the connected transaction history that quality and regulatory teams can use during an investigation; decisions about recall scope and regulatory actions remain part of the manufacturer’s approved procedures.
How does Business Central support quality management?
Quality management in Business Central changed significantly in 2026. Microsoft introduced Quality Management in Business Central 2026 release wave 1 as a Microsoft-published extension. It can create quality inspections at points in purchasing, production, assembly, and warehouse processes. The extension supports automatic, manual, and scheduled inspections, inspection templates, pass/fail criteria, lot blocking, workflows, and nonconforming item processing.
Manufacturers that previously relied on spreadsheets or separate inspection tools may now be able to bring more operational quality control directly into their ERP. See how quality management works in Dynamics 365 Business Central for a closer look at the functionality and its limitations.
Inspect incoming materials before they enter production
Business Central can create inspections around purchasing and receiving. Quality templates define measurements, attributes, acceptable ranges, and pass/fail criteria users need to record. This can give manufacturers a more consistent process for checking critical supplier components before they become available for production.
Inspect production output
Business Central can also create inspections around production output, connecting the manufacturing transaction with the related quality review. Manual inspections can support spot checks, investigations of a specific lot, or responses to a quality issue, while scheduled inspections can support recurring quality activities.

Block or quarantine nonconforming inventory
Recording a failed inspection is only useful if the business controls what happens next. Quality workflows can respond to inspection results by blocking tracked lots, serial numbers, or packages and moving affected inventory. Microsoft provides scenarios where a failed lot becomes blocked and inventory moves to a quarantine bin for further review.
A practical flow may look like:
Inspection → Pass → Release for use or shipment
or
Inspection → Fail → Block → Quarantine → Review → Disposition
These controls can reduce the risk of employees consuming or shipping inventory that failed a required inspection.
Quality Management does not automatically create a complete medical device quality system. Formal CAPA, advanced nonconformance management, controlled documentation, and other regulated processes may still require additional technology.
How can Business Central support medical device compliance, identification, and recalls?
Medical device requirements depend on where a company operates, where it sells products, its device classifications, and its role in the supply chain. A manufacturer serving the United States and Canada may need to design its ERP and surrounding quality systems around requirements in both countries.
Business Central can support traceability, transaction history, quality information, inventory records, and distribution data within that broader compliance environment.
For medical device manufacturers in the United States
Medical device manufacturers that sell devices in the United States are regulated by the U.S. Food and Drug Administration (FDA). The FDA oversees areas such as device classification, registration and listing, labeling, quality management requirements, reporting, recalls, and manufacturer inspections. The specific requirements depend on the device and its classification.
The FDA’s Quality Management System Regulation (QMSR) became effective February 2, 2026. It amended 21 CFR Part 820 and incorporates ISO 13485:2016 by reference. Manufacturers can review the FDA’s official Quality Management System Regulation guidance for current requirements.
Business Central can support operational records and processes used within an FDA-regulated manufacturer’s quality system, including:
- Production and traceability records: Connect purchased materials, lots, serial numbers, production consumption, output, and shipments.
- Quality records: Capture inspection measurements, pass/fail results, and related quality workflow actions.
- Recall investigation data: Trace affected materials through production and identify finished goods and customer shipments.
- UDI-related ERP data: Maintain item, lot, serial, expiration, and manufacturing information that may feed labeling or UDI processes.
- Change tracking: Use the configurable Change Log to record selected data changes, who made them, and when.
Business Central does not replace all FDA-related systems or processes. UDI labeling, GUDID submissions, electronic signatures, complaint handling, validation documentation, and other regulated requirements may still require additional applications, integrations, or controlled procedures.
For medical device manufacturers in Canada
Canadian medical device manufacturers must consider Health Canada’s Medical Devices Regulations and requirements associated with their device classifications. For applicable Class II, III, and IV manufacturers, Health Canada uses the Medical Device Single Audit Program, or MDSAP, for quality management system certification.
Business Central can support relevant operational records, including:
- Distribution records: Maintain customer, product, shipment date, quantity, location, and tracked-item information.
- Recall investigations: Trace affected lots or serial numbers through inventory, production, and customer shipments.
- Production records: Maintain material consumption, production output, inventory movements, and related transactions.
- Quality inspections: Keep operational inspection results connected with purchasing, production, and inventory.
- Cross-border traceability: Use the same ERP data foundation when products move through U.S. and Canadian supply chains.
Health Canada states that manufacturers, importers, and distributors must maintain distribution records for medical devices and that those records must contain enough information to support a rapid and complete recall. See Health Canada’s official guidance on medical device distribution records.
Manufacturers selling in both countries should map applicable U.S. and Canadian requirements before finalizing the solution design so that ERP data, quality systems, procedures, and controls work together.
How does Business Central support the broader medical device manufacturing process?
Traceability and quality are critical, but a medical device ERP also needs to run the business. Business Central connects manufacturing with purchasing, inventory, supply planning, warehousing, sales, costing, and finance, helping leaders manage regulated operational processes alongside delivery performance, working capital, capacity, and margins.
Manage production orders, BOMs, and routings
Production orders define what needs to be produced, how much is required, and when production should occur. Business Central connects the production BOM, routing, components, operations, and capacity requirements with the order.
BOMs define the components and subassemblies needed to build an item, while routings define the operations and resources required to manufacture it.

Plan materials and capacity
Business Central includes MPS and MRP planning capabilities that can use demand, inventory, lead times, BOM requirements, and existing supply to generate planning suggestions.
Connect inventory with purchasing and warehousing
Medical device manufacturers may manage raw materials, components, work in process, finished devices, spare parts, and quarantined stock across multiple locations.
Business Central connects purchasing, receiving, transfers, production consumption and output, inventory, picking, and shipment. Item tracking can continue across these processes when the appropriate tracking requirements are configured.
Connect production with financial performance
Business Central connects item and production activity with costing and financial management, giving finance and operations a shared view of inventory and manufacturing costs.
Manufacturers can analyze material and capacity costs, inventory valuation, production variances, scrap, finished goods costs, and margins. For additional insight, explore manufacturing reporting and analytics in Business Central.
How can Copilot and AI agents help medical device manufacturers using Business Central?
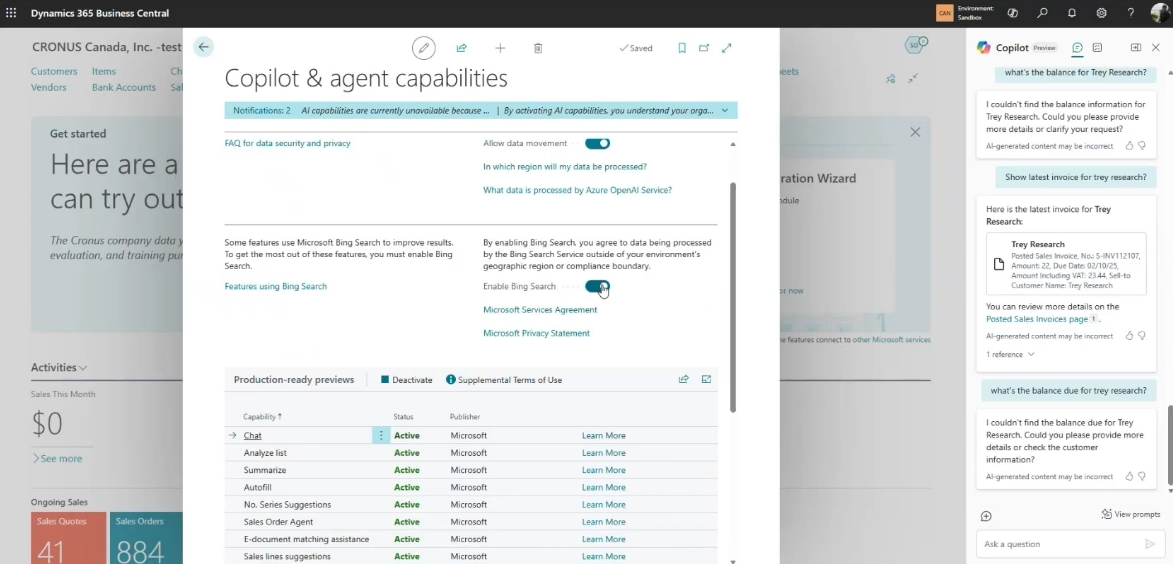
Copilot and AI agents can reduce administrative work and make Business Central information easier to use. For medical device manufacturers, a practical starting point is lower-risk processes where AI supports employees rather than making regulated quality decisions.
- Find ERP information faster: Chat with Copilot can help users locate Business Central records and information using natural language.
- Analyze operational data: Analysis Assist lets users describe how they want list data filtered, grouped, sorted, or summarized.
- Summarize records: Copilot can generate summaries of records such as customers, items, and sales orders for user review.
- Automate order administration: Sales Order Agent can help process emailed customer requests, identify customers and items, check availability, and prepare sales documents.
- Reduce accounts payable work: Payables Agent can process vendor invoice information and prepare purchase documents for review.
- Support defined workflows with custom agents: Custom Business Central agents can review ERP data, identify exceptions, summarize information, and prepare recommendations while keeping users involved in approvals.
Medical device manufacturers should establish clear AI governance. Product release, nonconformance disposition, recalls, regulatory reporting, and other controlled quality decisions should remain subject to approved procedures and appropriate human review.
Explore additional practical Copilot use cases in Business Central and custom AI agents for Business Central.

Understand Business Central pricing and licensing
Considering Business Central for your medical device manufacturing operation? Review the Business Central pricing and licensing guide to understand license options, costs, and factors that can affect the total ERP investment.
Where might medical device manufacturers need more than Business Central?
One of the most important implementation decisions is determining what belongs in the ERP and what belongs in a specialized application. Business Central now provides more operational quality functionality than it did before the 2026 release, but highly regulated manufacturers may still require additional technology.
From an implementation standpoint, we recommend treating Business Central Quality Management as an operational quality control layer, not automatically as a replacement for a complete regulated quality system. In our work configuring Business Central for manufacturers and distributors, we see the most value when inspections, receiving, production, and inventory controls share the same ERP data.
Formal CAPA, advanced regulated documentation, complex nonconformance workflows, and specialized compliance processes should be evaluated separately to determine whether an eQMS, extension, customization, or integration is the better fit.
Is Business Central a good fit for your medical device manufacturing company?
Business Central can be a strong option for medical device manufacturers that need more control than an accounting system or disconnected spreadsheets can provide without moving immediately to a large enterprise ERP.
Business Central may be worth considering when your organization:
- Is a small or midsize medical device manufacturer
- Primarily uses discrete manufacturing processes
- Needs stronger lot and serial traceability
- Wants production, quality, inventory, and finance connected
- Needs better purchasing and material planning
- Can integrate specialized quality or regulatory applications where required
The platform may be less appropriate when the organization has highly complex process or mixed-mode manufacturing, advanced global warehouse operations, high transaction volumes, or supply chain requirements that need greater enterprise depth.
In those situations, compare Business Central with Dynamics 365 Finance and Supply Chain Management. Our Dynamics 365 F&O vs. Business Central comparison explains the differences, while our guide to Dynamics 365 Finance and Supply Chain Management for complex manufacturing provides more detail on the larger platform’s manufacturing capabilities.
What should medical device manufacturers plan before implementing Business Central?
A regulated manufacturing ERP implementation should start with business and compliance requirements, not software screens.
Several planning decisions deserve attention early:
- Map regulatory requirements to system processes and controls. Identify what information employees must capture, who owns it, where it should live, and who can change it.
- Design lot and serial tracking before migrating inventory. Determine which raw materials, components, subassemblies, and finished devices require tracking.
- Define inspection points. Decide which suppliers, items, receipts, production outputs, or other events should trigger inspections.
- Map the complete traceability chain. Test the process from supplier receipt through production and customer shipment in both directions.
- Define system boundaries. Decide which processes belong in Business Central and which belong in an eQMS, MES, labeling platform, document system, CRM, or another application.
- Test exceptions, not just successful transactions. Include failed inspections, blocked lots, quarantine, supplier returns, rework, scrap, complaints, and recall scenarios.
- Include the right stakeholders. Quality, regulatory, production, warehousing, purchasing, finance, and IT should participate where their processes are affected.
Manufacturers that sell in both the United States and Canada should map requirements for both markets before finalizing solution design.
Our Business Central implementation guide provides additional planning guidance for requirements, data migration, integrations, testing, training, go-live, and adoption.
Plan your Business Central manufacturing solution
Evaluating Business Central for medical device manufacturing? Rand Group can help you assess manufacturing, traceability, quality, integration, reporting, and financial requirements and determine how Business Central should fit into your broader technology environment.
Why work with Rand Group for Business Central manufacturing?
Medical device ERP decisions cross finance, manufacturing, inventory, quality, reporting, and technology. Rand Group takes a cross-functional approach to Business Central implementation so these processes work together instead of being designed in isolation.
Our team supports Business Central manufacturing configuration, inventory and warehouse processes, integrations, custom development, reporting, training, and ongoing support. We also help organizations determine where standard Business Central functionality is enough and where an extension, integration, or specialized application makes more sense.
Hear what our clients say
“Without Business Central and Power Apps, we couldn’t keep up with what our customers expect. Now we can trace anything across the entire ecosystem, reduce waste, and make smarter business decisions quickly.” – Steven Chambers, Chief Financial Officer, Bartek Ingredients
“Working with Rand Group has been a game-changer for us. We felt supported the entire way, and whenever issues came up, the team was right there problem-solving with us.” – Danielle Johnson, Director of Data Systems, A-Z Process Solutions
Key takeaways
- Business Central can connect manufacturing, inventory, quality, traceability, purchasing, sales, and finance for small and midsize medical device manufacturers.
- Lot and serial tracking can help trace components through production and identify affected inventory and customer shipments during quality investigations.
- Business Central Quality Management adds inspections, pass/fail criteria, lot blocking, quarantine workflows, and other quality controls within the ERP.
- Business Central can support records and operational controls relevant to U.S. and Canadian medical device requirements, but ERP software alone does not make an organization compliant.
- Copilot and AI agents can reduce administrative work and improve access to ERP information, while regulated quality decisions should remain subject to defined controls and human oversight.
Frequently asked questions
Is Business Central a good ERP for medical device manufacturers?
Business Central can be a good ERP for small and midsize medical device manufacturers that need to connect finance, production, inventory, lot and serial traceability, purchasing, warehousing, and quality inspections.
Can Business Central track medical devices by lot and serial number?
Yes. Business Central supports serial, lot, and package number tracking. Its Item Tracing functionality can follow posted transactions forward and backward, helping manufacturers connect purchased materials, production consumption, finished output, inventory, and customer shipments.
Can Business Central help manufacturers manage medical device recalls?
Business Central can support recall investigations by tracing affected lots or serial numbers through purchasing, production, inventory, and customer shipments. Users can trace from a defective component to finished products that used it or start with a finished device and trace back through production and material origin. The ERP does not determine whether a recall is required. Manufacturers still need documented recall procedures and appropriate quality and regulatory oversight.
Does Business Central include quality management?
Yes. Microsoft introduced Quality Management in Business Central 2026 release wave 1. The extension supports automatic, manual, and scheduled inspections; templates and pass/fail criteria; lot blocking; workflows; and nonconforming item processing. More complex medical device quality requirements may still require an eQMS, extension, customization, or specialized application.
Can Business Central support FDA requirements for medical device manufacturers?
Business Central can support operational processes and records that may form part of an FDA-regulated manufacturer’s quality system, including production history, item traceability, quality inspections, inventory records, shipment information, and selected change logging. Compliance depends on the manufacturer’s complete quality system, procedures, validation approach, configuration, training, controls, and surrounding technology.
Can Business Central support Health Canada requirements for medical device manufacturers?
Business Central can support records and processes relevant to Canadian medical device operations, including lot and serial traceability, distribution information, customer shipments, inventory, production records, and quality inspections. The software can support the operational record, but it does not provide Health Canada, MDSAP, or ISO 13485 certification by itself.
Can Business Central replace an eQMS for a medical device manufacturer?
Not necessarily. Business Central Quality Management can manage operational quality processes such as incoming inspections, production output inspections, pass/fail criteria, lot blocking, scheduled inspections, quarantine, and workflow actions. A dedicated eQMS may still be needed for formal CAPA, complex nonconformance management, complaint handling, controlled documents, advanced approvals, training records, validation documentation, or other regulated processes.
How can Copilot and AI agents help medical device manufacturers?
Copilot and AI agents can help manufacturers find ERP data, analyze information, summarize records, and automate administrative processes such as sales order and accounts payable work. Medical device manufacturers should establish governance for AI use in regulated processes. Product release, quality disposition, recall, and regulatory decisions should follow approved procedures with appropriate human review.
Connect traceability, quality, manufacturing, and finance with Business Central
Medical device manufacturers need systems that connect suppliers, production, quality, inventory, customers, and finance. Dynamics 365 Business Central can provide that connected ERP foundation for many small and midsize manufacturers, with manufacturing, item tracking, inventory, and Quality Management capabilities that support traceability and visibility.
The right solution design should align with your processes, quality system, regulatory requirements, data, and surrounding applications. Contact Rand Group to discuss how Business Central can support your operations.